




Please Leave Us A Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.


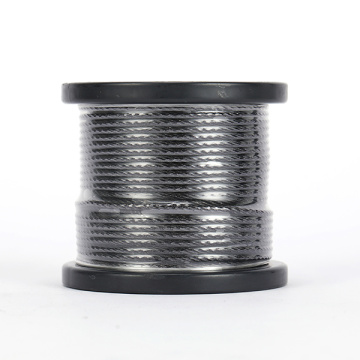




Gas shielded flux core welding wire is a specialized consumable designed for high-efficiency metal fabrication. Unlike solid wires that require external shielding gas from a cylinder, this tubular wire contains a flux core that generates its own protective gas atmosphere during the welding process. This unique design allows for deeper penetration and higher deposition rates, making it ideal for thick materials and outdoor environments where wind might disperse traditional shielding gas.
For industrial buyers, choosing the right flux cored arc welding (FCAW) wire means reducing downtime and increasing productivity. The self-shielding nature of these wires ensures consistent weld quality even in less-than-ideal conditions, providing a reliable solution for structural steel, shipbuilding, and heavy machinery manufacturing.
At Chenglu Stainless Steel Products Co., Ltd., every spool of gas shielded flux core welding wire undergoes rigorous testing to meet international standards. Our state-of-the-art production facility in Xinghua City utilizes advanced drawing equipment and precise flux blending technology to ensure uniform wire diameter and consistent chemical composition.
Multi-stage cold drawing processes ensure tight tolerances on wire diameter, preventing feeding issues in automated welding systems.
Spectrometric testing verifies that each batch meets exact specifications for carbon, manganese, and chromium content, guaranteeing mechanical properties.
Electropolishing and lubrication treatments reduce friction during welding, extending contact tip life and ensuring stable arc performance.
Selecting the correct gas shielded flux core welding wire requires matching the wire's classification to your base material, joint design, and welding position. Buyers should prioritize wires that offer smooth arc transfer, easy slag removal, and excellent impact toughness at low temperatures.
| Factor | Consideration | Buyer Benefit |
|---|---|---|
| Wire Classification | E71T-1, E70T-1, or E81T-N1 | Ensures compatibility with your specific steel grade and required tensile strength. |
| Diameter | 0.8mm, 1.0mm, 1.2mm, or 1.6mm | Larger diameters increase deposition rates for thick plates; smaller wires suit thin gauge work. |
| Shielding Gas | 75% Argon / 25% CO₂ (C75) | Optimizes arc stability and minimizes spatter, reducing post-weld cleaning time. |
| Pennant Style | Square vs. Round | Round pennants feed more reliably in automated systems; square may be cost-effective for manual welding. |
Before placing an order for bulk flux core welding wire, use this checklist to verify that your supplier can meet your operational requirements and quality expectations.
Request Mill Test Certificates (MTC) for every batch.
Verify AWS A5.20 or ISO 17633-A compliance.
Confirm availability of impact toughness data.
Check lead times for standard and custom orders.
Ensure secure packaging to prevent moisture absorption.
Verify export documentation capabilities for customs.
The versatility of gas shielded flux core welding wire makes it indispensable across multiple heavy industries. Its ability to handle dirty or rusty surfaces and its high deposition rate make it the preferred choice for structural fabrication and repair work.
Ideal for welding beams, columns, and bridges where high strength and speed are critical.
Used for thick plate welding in shipyards, offering deep penetration and resistance to porosity.
Essential for repairing and maintaining mining machinery exposed to abrasive wear and impact.
Facilitates rapid field repairs on pipelines due to its tolerance for wind and outdoor conditions.
Used in fabricating presses, conveyors, and heavy-duty frames requiring robust joints.
Perfect for maintenance shops dealing with varied thicknesses and surface conditions.
Sourcing welding consumables internationally often presents challenges related to quality consistency, logistics, and technical support. Understanding these common pitfalls helps buyers protect their operations and maintain supply chain efficiency.
Poor quality control in wire manufacturing can lead to erratic arc behavior, causing defects and rework.
Flux core wires are hygroscopic. Exposure to humidity during shipping can degrade weld quality, causing porosity.
Irregular wire diameter or burrs can cause birdnesting in automated welding robots, leading to production stoppages.
International buyers often struggle to get guidance on optimal welding parameters for new wire types.
When evaluating potential suppliers for gas shielded flux core welding wire, look for a partner that combines manufacturing expertise with a commitment to global quality standards. Chenglu Stainless Steel Products Co., Ltd. offers distinct advantages for international procurement.
Located in Xinghua City, Jiangsu Province, Chenglu specializes in high-quality stainless steel products, including welding wires. With advanced production equipment and an experienced technical team, they ensure every product meets international standards.
Their "integrity-based, innovation-based" corporate spirit drives continuous improvement in product structure and service quality. They are committed to becoming a global leading supplier, promoting industry progress through R&D investment and advanced technology adoption.
Get answers to common questions about gas shielded flux core welding wire sourcing, usage, and handling.
Gas shielded flux core wire requires an external shielding gas (typically C75: 75% Argon, 25% CO₂) to protect the weld pool, resulting in smoother arcs and less spatter. Self-shielded wire generates its own shielding from the flux core and does not require gas cylinders, making it better for windy outdoor conditions but often producing more spatter.
Store wire in a dry, climate-controlled environment. Keep it in its original sealed packaging until ready to use. If the package is opened, use the wire within 24 hours or store it in a drying oven at 100-120°C to remove moisture. Avoid storing near sources of heat or humidity.
Yes, one of the main advantages of flux core wire is its tolerance for minor surface contaminants. It can weld over light rust and paint better than solid MIG wire, though removing heavy scale and thick paint will still yield the best weld quality and reduce defects.
For most general purpose applications with ER70S-6 compatible flux cores, a mixture of 75% Argon and 25% CO₂ (often called C75 or ArCO₂) is recommended. This mix provides excellent arc stability, smooth bead appearance, and minimal spatter.
Buyers interested in testing our flux core welding wire quality should contact our sales team directly to discuss sample availability. We recommend testing small quantities before committing to large orders to ensure compatibility with your specific welding equipment and procedures.
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.