


Please Leave Us A Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.


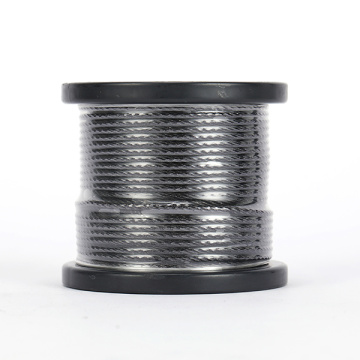


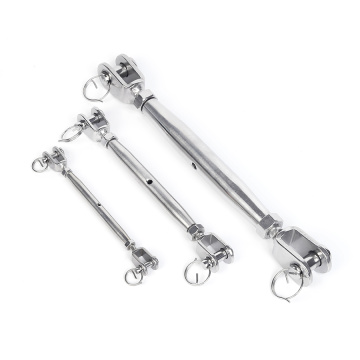


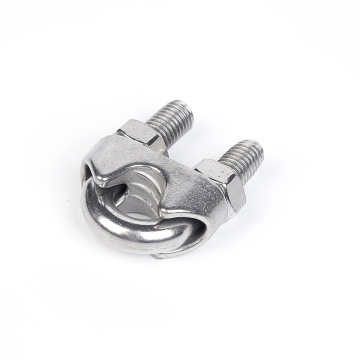

Black stainless steel cable is a specialized type of wire rope or cable that has been treated with a black oxide coating to enhance corrosion resistance while providing a sleek, modern aesthetic finish. Unlike standard stainless steel cables, the black oxide layer offers improved UV resistance and reduced glare, making it an ideal choice for applications where both durability and visual appeal are critical.
This material combines the inherent strength and longevity of stainless steel with the sophisticated appearance of a dark matte finish. For procurement buyers in construction, architectural design, and industrial sectors, choosing black stainless steel cable means investing in a product that requires minimal maintenance over its lifespan while delivering consistent performance under harsh environmental conditions. The black coating does not compromise the structural integrity of the underlying steel, ensuring reliable load-bearing capacity across various industries including food processing, pharmaceuticals, chemicals, and brewing.
Understanding the fundamental properties of black stainless steel cable helps streamline your sourcing decisions. When evaluating suppliers, prioritize those who use high-grade stainless steel substrates such as 304 or 316 grades, as these provide superior resistance to rust and chemical exposure. The black oxide process typically involves controlled oxidation at elevated temperatures, creating a stable magnetite layer that adheres tightly to the metal surface. This results in a durable finish that withstands abrasion, moisture, and temperature fluctuations without peeling or flaking.
Chenglu Stainless Steel Products Co., Ltd. operates from Xinghua City, Jiangsu Province, a region known for its advanced metallurgical industry and convenient logistics infrastructure. With years of dedicated focus on research, development, and production of high-quality stainless steel products, our facility leverages state-of-the-art equipment and experienced technical teams to ensure every batch meets international quality standards.
We adhere to a customer-centric service philosophy that prioritizes clear communication, transparent pricing, and flexible order fulfillment. Our team continuously optimizes product structures and improves service quality based on direct buyer feedback, reducing lead times and minimizing procurement risks. This commitment has earned us trusted partnerships with clients across multiple industries globally.
Our black stainless steel cables serve diverse sectors including food processing, pharmaceuticals, chemicals, brewing, and construction. The corrosion-resistant properties of our products make them suitable for environments exposed to moisture, chemicals, and high hygiene requirements. Buyers benefit from a single-source supplier capable of meeting varied specifications across different industry verticals.
Guided by the corporate spirit of "integrity-based, innovation-based," we consistently invest in R&D to introduce advanced technologies and management practices. This ongoing commitment ensures our black stainless steel cable offerings remain at the forefront of material science, providing buyers with cutting-edge solutions that lower total cost of ownership and enhance project outcomes.

Our manufacturing facility is equipped with advanced production lines and precision testing instruments designed to maintain tight tolerances and consistent output quality. Each stage of the black stainless steel cable production process — from raw material selection to final coating application — undergoes rigorous inspection protocols. This ensures dimensional accuracy, tensile strength compliance, and uniformity of the black oxide finish across every meter of cable produced.
An experienced technical team oversees all aspects of product development and quality assurance. Our engineers apply deep domain knowledge in stainless steel metallurgy and surface treatment processes to optimize formulations and production parameters. This expertise enables us to deliver black stainless steel cable that performs reliably in demanding applications, whether used in architectural installations, industrial rigging, or chemical processing environments.
Every product leaving our facility is tested to meet or exceed internationally recognized standards for stainless steel wire and cable. We conduct systematic checks for mechanical properties, corrosion resistance, and coating adhesion to guarantee that each shipment meets the exacting requirements of global buyers. This commitment to quality reduces risk for procurement teams and provides confidence in long-term product performance.
The first step in selecting a reliable supplier is confirming the base material grade of their black stainless steel cable. Premium grades such as AISI 304 and 316 offer distinct advantages in corrosive environments, with 316 providing enhanced resistance to chlorides and acidic substances. Request material test reports and verify that the supplier can trace raw materials back to certified mills. A supplier who proactively provides documentation demonstrates transparency and reduces verification costs for your procurement team.
Evaluate the supplier's manufacturing capacity to ensure they can handle your order volume without compromising quality or delivery schedules. Suppliers with well-established production lines and buffer inventory capabilities are better positioned to accommodate urgent requests and scale orders during peak demand periods. Clear communication about lead times and production milestones helps you plan downstream operations more effectively and avoid costly project delays.
A robust quality control system is non-negotiable when sourcing black stainless steel cable. Inquire about the supplier's inspection procedures, including incoming material checks, in-process monitoring, and final product testing. Suppliers who implement statistical process control and maintain detailed quality records provide greater assurance of consistency. Look for suppliers who welcome third-party inspections or audits, as this openness signals confidence in their manufacturing capabilities.

Confirm that the supplier's black stainless steel cable matches your required grade (304, 316, etc.), diameter, tensile strength, and length specifications. Misalignment here leads to costly rework and project delays.
Request evidence of black oxide coating adhesion tests and corrosion resistance data. Ensure the finish will withstand your intended environment without premature degradation or discoloration.
Research the supplier's history, client references, and industry reputation. Established manufacturers with proven export experience reduce the risk of supply chain disruptions and quality inconsistencies.
Ensure quotes include all cost components — material, processing, packaging, and shipping. Hidden fees inflate your landed cost and undermine budget accuracy. Compare unit prices across multiple qualified suppliers.
Verify that the supplier uses appropriate packaging to prevent damage during transit. Proper coiling, wrapping, and palletizing protect the black oxide finish and ensure products arrive in optimal condition.
Confirm the availability of technical support, replacement policies, and responsive communication channels. A supplier who stands behind their products provides peace of mind and resolves issues swiftly.
One of the most frequent issues buyers encounter is uneven or patchy black oxide coating across different batches. This inconsistency often stems from inadequate process control or rushed production cycles. To mitigate this risk, specify coating thickness tolerances in your purchase agreement and request sample approvals before committing to large orders.
Supply chain delays frequently disrupt project timelines, especially when buyers work with suppliers lacking transparent production tracking. Establish regular update cadences, define clear milestone dates, and require advance notice of any potential delays. Proactive communication prevents surprises and allows you to adjust downstream schedules accordingly.
Receiving cable marked as 316 stainless steel but delivered as lower-grade 304 is a serious quality breach that compromises end-product performance. Always insist on mill certificates and independent third-party testing for critical orders. Reputable suppliers like Chenglu provide full material traceability and welcome verification by external laboratories.
Improper packaging can result in kinked, tangled, or scratched cable upon arrival, rendering it unsuitable for installation. Specify packaging requirements upfront and confirm that the supplier uses protective wrapping and rigid containers. Insurance coverage for shipped goods further protects your investment against transit-related losses.
Prioritize suppliers who own their manufacturing facilities rather than trading companies. Direct manufacturers have greater control over quality, pricing, and lead times. Verify production capacity through facility tours, video walkthroughs, or third-party audit reports to confirm operational authenticity.
Suppliers with documented quality management systems demonstrate a structured approach to consistency and continuous improvement. Look for ISO-certified operations, standardized inspection checklists, and corrective action procedures. These systems reduce variability and ensure every shipment meets your specifications.
Experience serving international markets indicates familiarity with diverse regulatory requirements, cultural expectations, and logistical complexities. Suppliers with a track record of successful exports understand documentation needs, customs compliance, and cross-border communication protocols essential for smooth transactions.
Fast, accurate responses to inquiries and issue resolution are hallmarks of a professional supplier. Evaluate response times during the pre-sales phase as an indicator of post-order support quality. Suppliers who assign dedicated account managers streamline communication and build stronger buyer-supplier relationships.
While price should never be the sole deciding factor, competitive and transparent pricing reflects efficient operations and fair business practices. Compare total landed costs — including shipping, duties, and insurance — rather than unit prices alone. Suppliers offering volume discounts and flexible payment terms add measurable value to your procurement strategy.
Your projects may require specific diameters, lengths, or custom coil configurations. Suppliers who accommodate customization requests without excessive minimum order quantities enable you to optimize inventory and reduce waste. Discuss your unique requirements early to confirm feasibility and pricing implications.
Black stainless steel cable features a black oxide coating applied to the surface of standard stainless steel wire or cable. This coating provides enhanced corrosion resistance, improved UV stability, and a visually appealing dark matte finish that reduces light reflection. While the underlying steel composition remains the same — typically 304 or 316 grade — the black oxide layer adds an extra protective barrier against moisture, chemicals, and environmental exposure. For buyers, this means longer service life in outdoor or chemically aggressive environments combined with a modern aesthetic suitable for architectural and design-focused applications.
Yes, black stainless steel cable is highly suitable for outdoor construction applications. The black oxide coating significantly enhances resistance to weathering, rain, humidity, and UV radiation compared to bare stainless steel. When paired with marine-grade 316 stainless steel, the cable delivers exceptional performance in coastal or high-salinity environments. Architects and contractors increasingly specify black stainless steel cable for railing systems, tensioned wire installations, and decorative structural elements where both durability and visual sophistication are required.
Under normal operating conditions, the black oxide coating on stainless steel cable is remarkably durable and resistant to wear. The coating forms a stable magnetite layer that bonds chemically with the steel substrate, making it difficult to peel or flake. However, extreme abrasive conditions — such as constant friction against rough surfaces or exposure to highly acidic cleaning agents — can gradually degrade the finish over extended periods. For most architectural, industrial, and rigging applications, the coating maintains its appearance and protective qualities throughout the cable's functional lifespan without requiring maintenance or recoating.
Minimum order quantities vary depending on the supplier, cable specifications, and production scheduling. Many established manufacturers, including Chenglu Stainless Steel Products Co., Ltd., offer flexible MOQs to accommodate both small trial orders and large-scale procurement needs. Typical MOQs range from 500 kg to 2,000 kg, though custom configurations may require higher volumes due to setup costs. Buyers should discuss their projected annual requirements with the supplier to negotiate favorable terms, volume discounts, and consolidated shipping arrangements that reduce per-unit costs.
Before committing to a bulk order, request physical samples and review comprehensive documentation including material test reports, coating adhesion test results, and corrosion resistance data. Conduct your own independent testing if possible, particularly for critical applications. Visit the manufacturing facility or arrange a virtual tour to assess production capabilities and quality control processes. Reputable suppliers will readily provide samples, documentation, and access to their operations, demonstrating confidence in their product quality and manufacturing standards.
Professional suppliers employ multi-layer packaging strategies to protect black stainless steel cable during transit. Common methods include inner plastic wrapping to prevent moisture ingress, outer kraft paper or woven bags for abrasion resistance, and secure wooden crates or steel-reinforced pallets for heavy shipments. Coils are typically strapped and padded to prevent shifting, while cut-length cables are bundled and individually wrapped. These measures preserve the integrity of the black oxide finish and ensure products arrive in pristine condition ready for immediate installation.
Yes, reputable manufacturers produce black stainless steel cable in compliance with international standards governing stainless steel wire, wire rope, and surface treatment processes. Products are tested for tensile strength, elongation, bend radius, and coating adherence against benchmarks set by organizations such as ASTM, EN, and JIS. Suppliers who maintain documented quality management systems and provide third-party certification reports give buyers confidence that their black stainless steel cable meets the rigorous safety and performance requirements of global markets and regulated industries.
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.